
AXALLOY Precision
5-Axis Prototype Machining
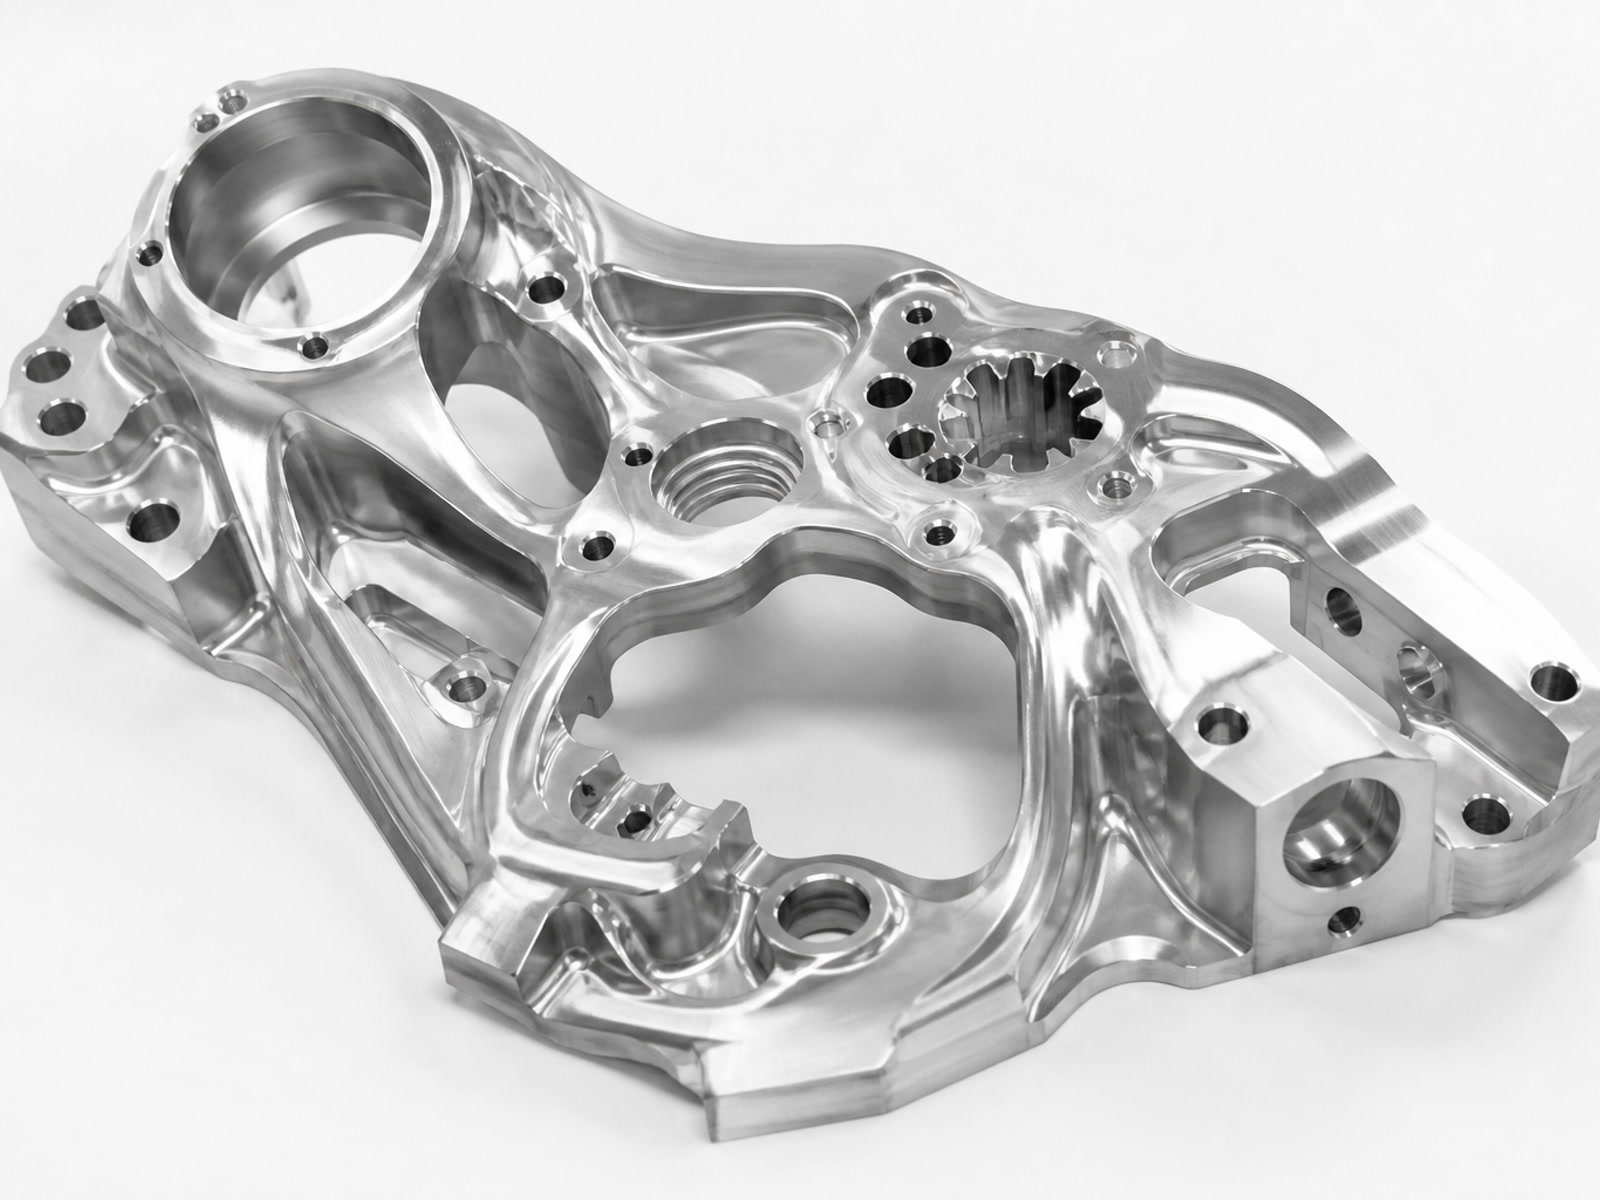
AXALLOY Precision provides 5-axis prototype machining for complex, high-value parts made from difficult-to-machine alloys. Based in Shenzhen, we support international engineering, procurement, and quality teams from early design validation through controlled repeat production—especially when geometry, tolerances, and documentation requirements leave little margin for error.
Why 5-Axis Prototypes with AXALLOY
5-axis machining is often the fastest route to accurate prototypes when parts include compound angles, sculpted surfaces, deep pockets, thin walls, or critical feature relationships. Our approach emphasizes manufacturability, process control, and inspection planning—so your prototype is not just "a one-off," but a credible first step toward stable production.
Best For:
- Complex contours and multi-face features requiring fewer setups
- Tight GD&T and precision interfaces where alignment matters
- Prototypes that must transition cleanly into low-volume or repeat builds
- Difficult alloys where toolpath strategy and cutting stability are critical
Typical Customer Fit
AXALLOY is a strong fit for teams that prioritize manufacturability feedback, dependable communication, and quality evidence—not just the lowest unit price.
Industries
- Aerospace
- Medical devices
- Semiconductor equipment
- Energy, oil & gas, marine
- Robotics, automation
- Precision industrial equipment
Decision-Makers We Support
- Mechanical/design/manufacturing engineers — DFM + tolerance review
- Procurement/sourcing — risk, delivery, responsiveness, capability
- Quality — traceability, FAI, dimensional reporting, controlled records
Difficult-Alloy Prototype Materials We Machine
We specialize in prototypes for alloys that punish poor process planning. If your drawing calls out a specific heat/condition, we can align machining and inspection strategy accordingly.
Nickel Alloys
Inconel 718/625, Inconel 600/601/690, X-750, 725
Hastelloy
C-276, C-22, B-2
Monel
400, K-500
Titanium
Grade 2, Grade 5, Grade 23
Stainless Steels
316L, 17-4 PH, 15-5 PH, 304, 321
Duplex
2205, Super Duplex 2507
Cobalt Alloys
MP35N, Cobalt Chrome, L605
Other Specialty Metals
A286, Nitronic 50/60, Nitinol, molybdenum, tungsten, copper-nickel
5-Axis Prototype Machining Capabilities
Machining Envelope & Precision
- Max 5-axis part size
- Ø500 × 400 mm
- Positioning accuracy
- ±0.005 mm
- Repeatability
- ±0.003 mm
- Typical milling tolerance
- down to ±0.005 mm
- Min. internal corner radius
- R0.3 mm
- Min. wall thickness
- 0.5 mm
- Standard surface finish
- Ra 1.6 μm
- Precision machined finish
- Ra 0.8 μm
- Ground finish (as required)
- down to Ra 0.2 μm
Prototype Quantities & Lead Time
- Prototype quantity
- 1–20 parts
- Prototype lead time
- 5–10 business days
- Expedited service
- Available
- Minimum order quantity
- 1 part
From Prototype to Repeatable Process: Before cutting metal, we evaluate material behavior, geometry risk, tolerances, GD&T, surface finish, inspection method, and planned volume. We provide DFM feedback, tolerance review, and fixture/process planning for smooth transition into low-volume production.
Inspection, Traceability & Documentation
For prototype programs with aerospace/medical/semicon expectations, we support export-ready documentation and project-specific quality records.
Inspection Capabilities
- CMM range
- 700 × 1,000 × 600 mm
- CMM accuracy
- up to 1.8 + L/300 μm
- Optical measurement accuracy
- ±0.002 mm
- Surface roughness measurement
- Ra 0.05–40 μm
- Hardness testing
- Rockwell, Brinell, Vickers
- Environment
- Temp-controlled room; calibrated equipment
Common Quality Deliverables
- Material Test Report / Mill Test Certificate
- Certificate of Conformance (CoC)
- First Article Inspection (FAI) report
- Ballooned drawing + full dimensional report
- Surface roughness report
- Heat treatment and coating certificates (when applicable)
- Material and lot traceability; special process records
Related Processes to Support 5-Axis Prototypes
When prototypes require more than milling, we coordinate supporting processes to reduce handoffs and setup risk:
- Turning and mill-turn for hybrid components
- Wire EDM / sinker EDM for sharp internal features and deep cavities
- Precision grinding for tight fits and low Ra surfaces
- Heat treatment, passivation, coating, deburring, marking, cleaning, and assembly support
What Makes a Prototype RFQ "Strong"
To quote accurately and build the right process route, ideal inputs include:
- 1.2D drawing (with GD&T) + 3D model
- 2.Defined material grade and condition
- 3.Critical features identified (datums, fits, sealing surfaces, etc.)
- 4.Quantity (prototype + expected follow-on volume)
- 5.Required documentation (FAI, MTR, dimensional report, etc.)
- 6.Target delivery date and any packaging requirements
Supported File Formats
Request a 5-Axis Prototype Machining Quote
If your prototype involves difficult alloys, tight tolerances, or complex 5-axis geometry, send your drawing/model and requirements. We'll review manufacturability, confirm inspection strategy, and propose a stable machining route aligned with your prototype goals and next-step production needs.
- DFM feedback and tolerance review included
- Material and inspection strategy confirmation
- Responses within 24–48 hours