
AXALLOY Precision
Complex Cavity EDM
AXALLOY Precision provides complex cavity EDM services for high-value components in difficult-to-machine alloys. Based in Shenzhen and supporting international engineering, procurement and quality teams, we combine sinker EDM, wire EDM, precision grinding and CNC machining to deliver deep cavities, blind features, sharp internal corners and precision profiles with controlled tolerances, documented quality and dependable communication.
We are best suited to customers who value manufacturability, process control, traceability and complete documentation—rather than the lowest unit price alone.
What We Mean by Complex Cavity EDM
Complex cavity EDM encompasses features that are difficult or impractical to machine via conventional cutting. Our process engineers evaluate each geometry to determine the optimal EDM method, electrode strategy and finishing approach.
- Deep, narrow cavities and ribs with high aspect ratios
- Blind internal forms requiring tight corner radii
- Sharp internal corners and thin web sections
- Precision profiles in hardened or heat-resistant alloys
- Features demanding minimal tool pressure, reduced burrs or low distortion
- Surfaces requiring uniform micro-finishes without tool marks
By selecting between sinker EDM for deep and blind cavity formation and wire EDM for through profiles and sharp internal geometry, we define a controlled process that balances tolerance, surface finish and lead time.
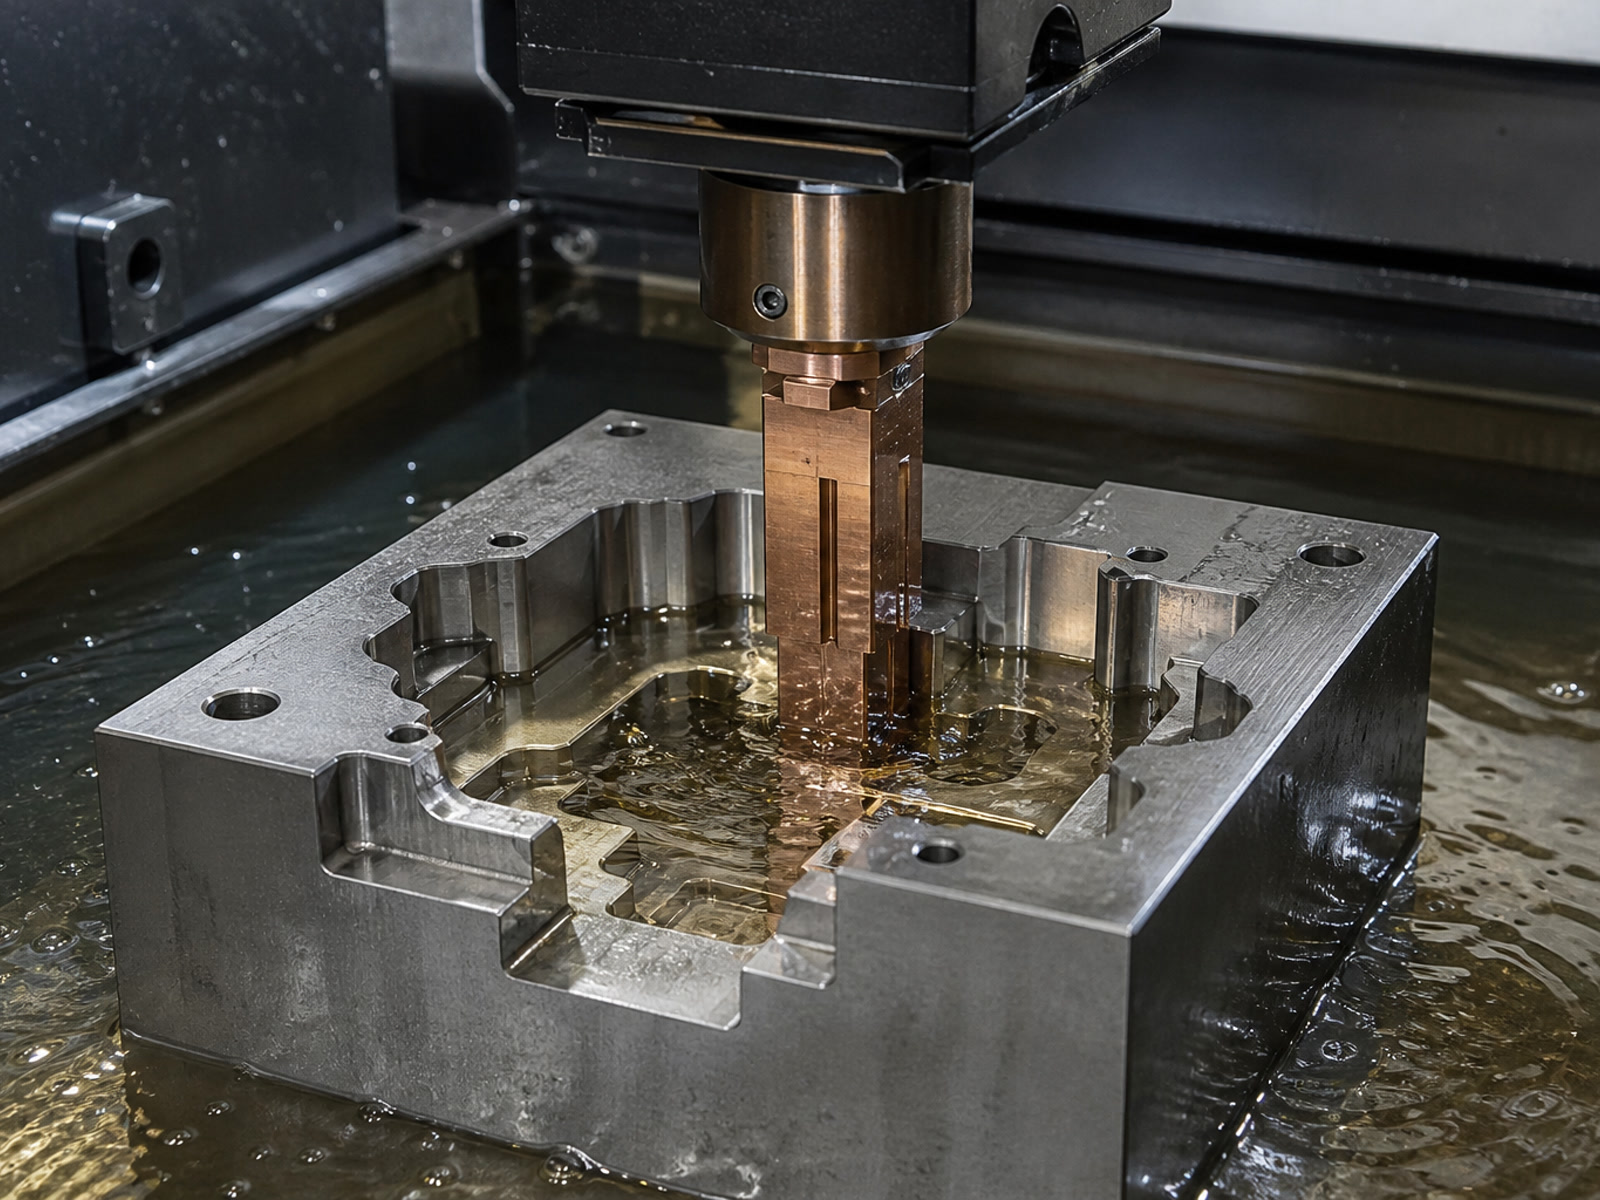
Core EDM Capabilities
Two complementary EDM technologies, each with specific strengths for complex cavity work.
Sinker EDM
For deep cavities, ribs, blind features and complex internal profiles.
- Max workpiece size500 × 350 × 300 mm
- Max workpiece weight800 kg
- Positioning accuracy±0.005 mm
- Repeatability±0.003 mm
- Min internal corner radiusR0.05 mm
- Max machining depth250 mm
- Surface finishdown to Ra 0.4 μm
- Best suited forDeep cavities, internal pockets, thin ribs, undercuts, blind features
Wire EDM
For sharp internal corners, narrow slots and precision profiles.
- Max workpiece size600 × 400 × 300 mm
- Max workpiece weight500 kg
- Wire diameterØ0.10–0.30 mm
- Min cutting width0.15 mm
- Cutting accuracydown to ±0.005 mm
- Repeatability±0.003 mm
- Max cutting taper±30°
- Surface finishdown to Ra 0.8 μm
- Max cutting thickness300 mm
- Best suited forSharp internal corners, narrow slots, punches/dies, precision inserts
Complementary Processes
Beyond EDM, we integrate additional precision processes for complete part delivery.
Precision Grinding
- Surface finish down to Ra 0.2 μm
- Flatness to 0.003 mm
- Roundness to 0.002 mm
- Grinding tolerance down to ±0.002 mm
CNC Milling & Turning
- 3-, 4-, 5-axis milling
- Turning and mill-turn
- Pre/post-op stock preparation
- Datum definition and assembly interfaces
Special Processes
- Heat treatment
- Passivation and coatings
- Deburring, marking and cleaning
- Assembly support
Difficult Alloys and Specialty Metals
We specialize in complex cavity EDM for challenging materials across eight major alloy families.
Nickel-Based Superalloys
Inconel 600/601/625/690/706/718/725, X-750; Hastelloy C-22, C-276; Monel 400, K-500; Waspaloy, Nimonic
Cobalt Alloys
Stellite, L605, MP35N, cobalt chrome
Titanium Alloys
Grades 2, 5, 9, 12, 23
Stainless Steels
15-5 PH, 17-4 PH, 316L, 304, 321, 410, 420, 440C
Duplex & Super Duplex
2205, 2507
High-Temperature Steels
A286, Nitronic 50/60
Specialty Metals
Nitinol, molybdenum, tungsten, copper-nickel alloys
Tool Steels
A2, D2, H13, M2
Tolerances and Surfaces
Dimensional Control
- EDM dimensional accuracydown to ±0.005 mm
- Repeatability±0.003 mm
- Min internal corner radius (sinker)R0.05 mm
- Min cutting width (wire)0.15 mm
Surface Finishes
- Sinker EDMdown to Ra 0.4 μm
- Wire EDMdown to Ra 0.8 μm
- Precision grounddown to Ra 0.2 μm
Geometric Control Supported
- Flatnessdown to 0.003–0.005 mm
- Concentricitydown to 0.008 mm
- Position tolerancedown to 0.010 mm
Note: Achievable tolerances depend on geometry, material, cavity depth and flushing strategy. We review these factors upfront before fixing the process route.
Where Complex Cavity EDM Is a Best Fit
Proven across demanding industries and component types.
Industries
Typical Components
- Turbine and combustor hardware: cooling channels, diffuser pockets, fir-tree root features
- Medical and surgical tools: deep slots, implant cavity forms, ultra-fine ribs
- Semiconductor tooling and fixtures: precision inserts, micro-features, vacuum channels
- Valve and flow-control systems: nozzle cavities, metering slots, internal sealing features
- Mold and die inserts for specialty alloys or high-temperature applications
Process Approach
We evaluate each project across seven key dimensions before committing to a process route:
- Material behavior and heat treatment state
- Cavity geometry, depth, aspect ratios and venting paths
- Required corner radii and finishes
- Datum strategy and inspection plan (CMM, optical)
- Production volume and repeatability requirements
- Documentation and traceability needs
Typical Workflow
-
1
RFQ Submission
Submit 3D model, 2D drawing and defined material
-
2
DFM & Tolerance Review
Identification of critical features and surfaces
-
3
Process Plan
Pre-EDM stock prep, electrode strategy, flushing and finishing
-
4
Pilot / FAI Run
With full documentation if required
-
5
Controlled Repeat Production
With in-process inspection and final reporting
Engineering Support and DFM Guidelines
We provide drawing reviews, tolerance and process feedback, fixture planning and documentation alignment before production.
Electrode Strategy
- Graphite or copper electrodes selected based on finish, detail and material
- Allow for spark gap and overburn; typical 0.01–0.05 mm depending on finish and material
- Multi-electrode staging for deep or high-aspect cavities to manage wear and maintain geometry
Flushing and Venting
- Provide flushing ports or consider temporary EDM holes when possible
- Design vent paths to avoid recast and achieve consistent finishes at depth
Corner Radii and Webs
- R0.05 mm is achievable with sinker EDM; confirm material and aspect ratio
- Maintain minimum web thickness and support features to limit deflection
Datum and Inspection
- Define datum features accessible post-EDM
- Include profile/position tolerances and critical surfaces on 2D drawings
Finishing
- Combine EDM with precision grinding or lapping for sealing surfaces and bearing fits
- Plan for passivation/coatings where corrosion or biocompatibility is critical
Inspection and Documentation
Temperature-controlled inspection room with calibrated equipment and complete quality documentation.
Inspection Capabilities
- CMM measuring range700 × 1,000 × 600 mm
- CMM accuracyup to 1.8 + L/300 μm
- Optical measurement accuracy±0.002 mm
- Height gauge resolution0.001 mm
- Surface roughness rangeRa 0.05–40 μm
- Hardness testingRockwell, Brinell, Vickers
Quality Documentation
- Material test reports and mill certificates
- Certificate of Conformance
- First Article Inspection reports with ballooned drawings
- Full dimensional inspection reports
- Surface roughness, heat treatment and coating certificates
- Material and lot traceability
- Special process records and inspection photos upon request
- Custom documentation packages available
Capacity, Lead Times and Volumes
Flexible production from single prototypes to high-volume batch runs.
1–20
Prototype Parts
Lead time: 5–10 business days
20–500
Low-Volume
Lead time: 10–20 business days
500–10,000+
Batch Production
Expedited service available
Key Limits
- Minimum order quantity: 1 part
- Max workpiece weight: 800 kg (sinker), 500 kg (wire)
- Integration with multi-axis milling, turning, mill-turn and grinding for efficient hybrid routing
Supported Volume
Production volume from 1 to 10,000+ parts with controlled repeatability and full documentation at every stage.
File Formats and RFQ Inputs
Send us your design files in the format that works best for you.
Accepted File Formats
- Max upload per RFQ: 500 MB
- Drawing units: millimeters or inches
Best-Fit RFQ Package
- 3D model and fully dimensioned 2D drawing with tolerances and datums
- Material grade and condition; required heat treatment
- Identified critical features, surfaces and inspection criteria
- Quantities by lot/run; target delivery date
- Required documentation (FAI, CoC, MTRs, special-process certs)
- Packaging and export requirements
Why AXALLOY for Complex Cavity EDM
Difficult Alloys, Controlled Processes
Proven routing for Inconel, Hastelloy, titanium, duplex and cobalt alloys
Tight Tolerances and Finishes
Sinker EDM to Ra 0.4 μm; precise profiles and deep features with repeatability
Hybrid Capability
EDM + multi-axis milling + grinding for complete parts and datum control
Documentation-First Mindset
FAI, dimensional reports, traceability and export-ready documentation
Communication and Stability
Clear DFM feedback, realistic schedules and dependable quality for repeat programs
Frequently Asked Questions
When should I choose EDM over 5-axis milling?
EDM is preferred for deep, narrow cavities; sharp internal corners; very fine radii; thin webs; hardened or high-temperature alloys; and when low cutting forces and burr-free features are critical.
What surface finishes can you achieve on EDM cavities?
Sinker EDM down to Ra 0.4 μm; wire EDM down to Ra 0.8 μm. For sealing surfaces, we can follow with precision grinding or lapping down to Ra 0.2 μm.
What is the smallest internal corner you can produce?
Sinker EDM minimum internal corner radius is R0.05 mm, pending material and aspect ratio.
How do you manage deep cavities?
We balance electrode design, staged roughing/finishing, controlled flushing and thermal management; and we validate with in-process inspection and finishing passes.
Can you provide FAI and full dimensional reports?
Yes. We support FAI, ballooned drawings, full dimensional reports, material traceability and special-process records.
Get a Quote
Send your RFQ with 3D CAD and 2D drawings, material specification and required documentation. We will review manufacturability, propose a stable EDM process, and return a detailed quote and delivery plan.
AXALLOY Precision supports international programs from prototype through controlled repeat production—especially where complex cavity EDM, tight tolerances and difficult alloys converge.