
Precision Machining for Cupro Nickel 90/10 (UNS C71500 / C70600)
CuNi 90/10 Machining Services
AXALLOY Precision — Shenzhen-based CNC machining partner specializing in complex, high-value components made from difficult-to-machine alloys. We support international engineering, procurement and quality teams from prototype development through low-volume and repeat production.
We evaluate material behavior, geometry, tolerances, surface requirements, inspection strategy and production volume before defining the machining process.
Request a QuoteWhy AXALLOY for CuNi 90/10 Machining?
CuNi 90/10 (copper-nickel alloy 90% Cu / 10% Ni, UNS C71500) offers outstanding corrosion resistance in seawater and biofouling, plus excellent thermal conductivity and mechanical strength — making it ideal for marine, chemical, offshore, heat exchanger, condenser, and petrochemical applications. However, it requires careful handling due to its work-hardening tendency and high ductility.
We excel where others do not:
- Proven experience with difficult alloys including copper-nickel, nickel-based superalloys, titanium, and cobalt alloys.
- Consistent process control, material traceability, and documentation — exactly what your quality, engineering, and procurement teams demand.
- Supported by our complete facility: multi-axis CNC milling (3/4/5-axis), turning, mill-turn, Swiss CNC, Wire EDM, Sinker EDM, and precision grinding.
- Aerospace / marine / energy / robotics customers trust us for complex geometry, thin walls, critical interfaces, and tight tolerances.
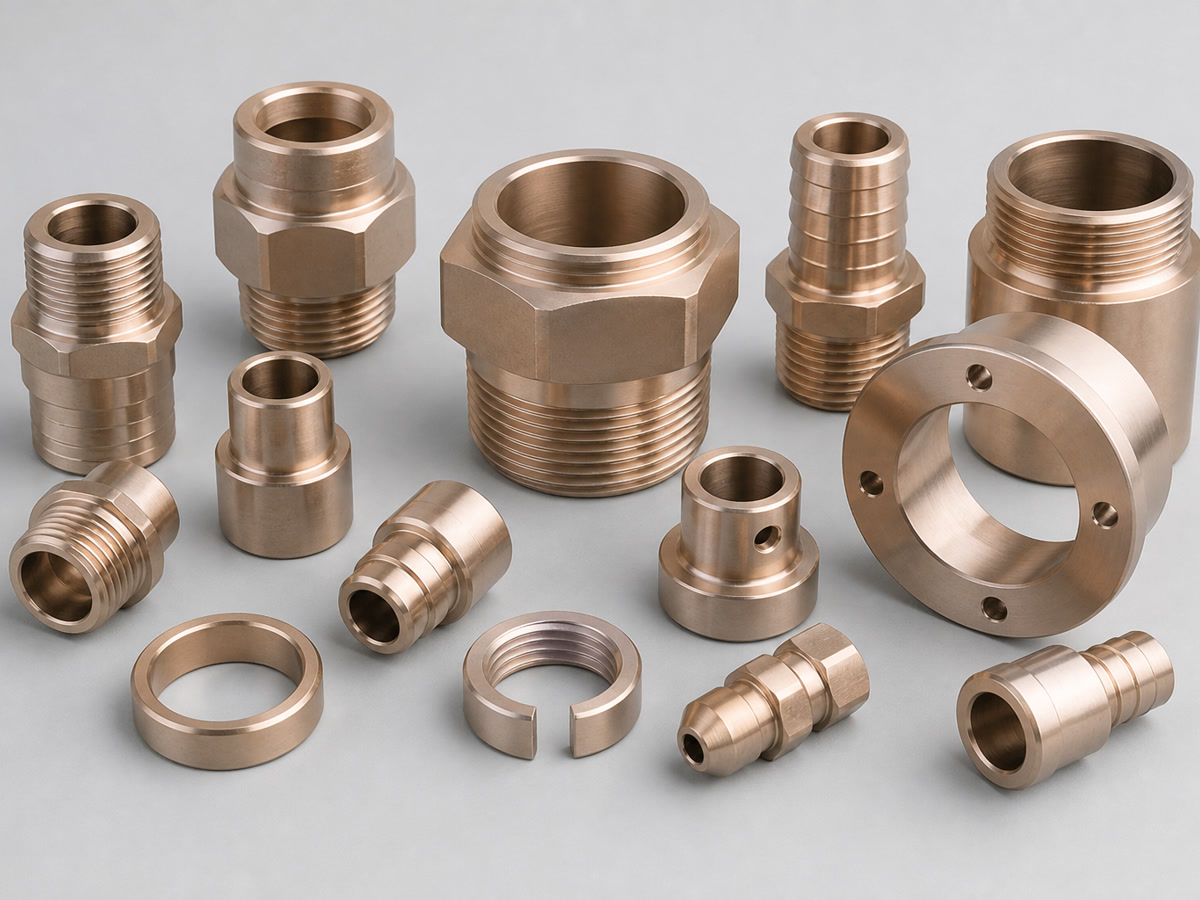
Our Machining Capabilities for CuNi 90/10
| Process | Key Strengths & Capabilities |
|---|---|
| 3-Axis / 4-Axis / 5-Axis Milling | Complex contours, pockets, thin walls, precision interfaces. Max part size up to 1,000 × 600 × 600 mm. |
| Turning & Mill-Turn | Shafts, nozzles, fittings, valve bodies. Up to 9 controlled axes. |
| Swiss CNC Turning | Small-diameter precision fittings, pins, connectors (Ø0.5–32 mm). |
| Wire EDM / Sinker EDM | Narrow slots, sharp internal corners, blind features, precision inserts (Ra 0.4–0.8 μm). |
| Precision Grinding | Shafts, sealing surfaces, bearing fits (Ra 0.2 μm, ±0.002 mm). |
| Assembly & Special Processes | Deburring, passivation, coating, heat treatment, cleaning. |
Standard Tolerances
- Dimensional:±0.005 mm (precision)
- Angular:±0.1°
- Flatness:down to 0.005 mm
- Concentricity:down to 0.008 mm
- Surface Finish:Ra 0.8 μm (precision), down to Ra 0.2 μm (ground)
Supported File Formats
STEP, STP, IGES, X_T, X_B, SLDPRT, SAT, PDF, DWG, DXF (up to 500 MB per RFQ).
Lead Times
- Prototypes: 5–10 business days
- Low-volume production: 10–20 business days (expedited service available)
Recommended Machining Practices for CuNi 90/10
Tooling
- Coated carbide (TiN/TiAlN) or PCD with positive rake angles and chip-breaking geometries.
- Avoid dwell time; use sharp tools to prevent work hardening.
Cutting Parameters
- Cutting speed: 100–200 m/min (carbide)
- Feed rate: 0.05–0.2 mm/rev
- Depth of cut: 0.1–2 mm (shallow for finishing)
- Climb milling preferred to reduce work hardening.
Cooling & Lubrication
- High-pressure coolant (sulfur-free) to control heat and chip evacuation.
- Maintain workpiece temperature to minimize hardening.
Best Practices
- Sharp tools + consistent parameters = minimal work hardening.
- Anneal or stress-relieve when possible for larger or more complex parts.
- Full material traceability and first-article inspection on every job.
Quality & Documentation
- CMM (700 × 1,000 × 600 mm)
- Material certificates, mill test reports, first-article inspection reports
- Ballooned drawings, surface roughness reports, heat-treatment/coating certificates
- Temperature-controlled inspection room
- Full traceability and custom quality plans
Minimum Order Quantity: 1 part
Industries & Projects We Serve Best
Ideal for
- Marine & offshore (valve seats, propellers, piping)
- Heat exchangers & condensers
- Petrochemical & chemical processing equipment
- Precision electrical / instrumentation components
- Complex assemblies requiring thin walls and tight tolerances
Not ideal for
- Commodity parts bought solely on lowest price
- Incomplete drawings or unverified material certification
- Unauthorized reproduction of existing designs
Strong project inputs we love
- Complete 2D drawings + 3D models
- Defined CuNi 90/10 grade and critical features
- Target quantities and realistic delivery date
- Required documentation and export-ready packaging
Ready to Quote Your CuNi 90/10 Project?
Upload your drawings (STEP/IGES/X_T preferred) or send us an RFQ with part description, material specification, quantities, and critical requirements.
AXALLOY Precision
Shenzhen, China
CNC machining for difficult alloys — precision you can trust.
Contact our engineering team for free DFM feedback on any CuNi 90/10 project.