
Inconel vs Hastelloy CNC Machining
Prototype to Low-Volume Production with Full Documentation
We precision machine complex Inconel and Hastelloy components from prototype through controlled repeat production — with dependable communication, process control and export-ready quality records.
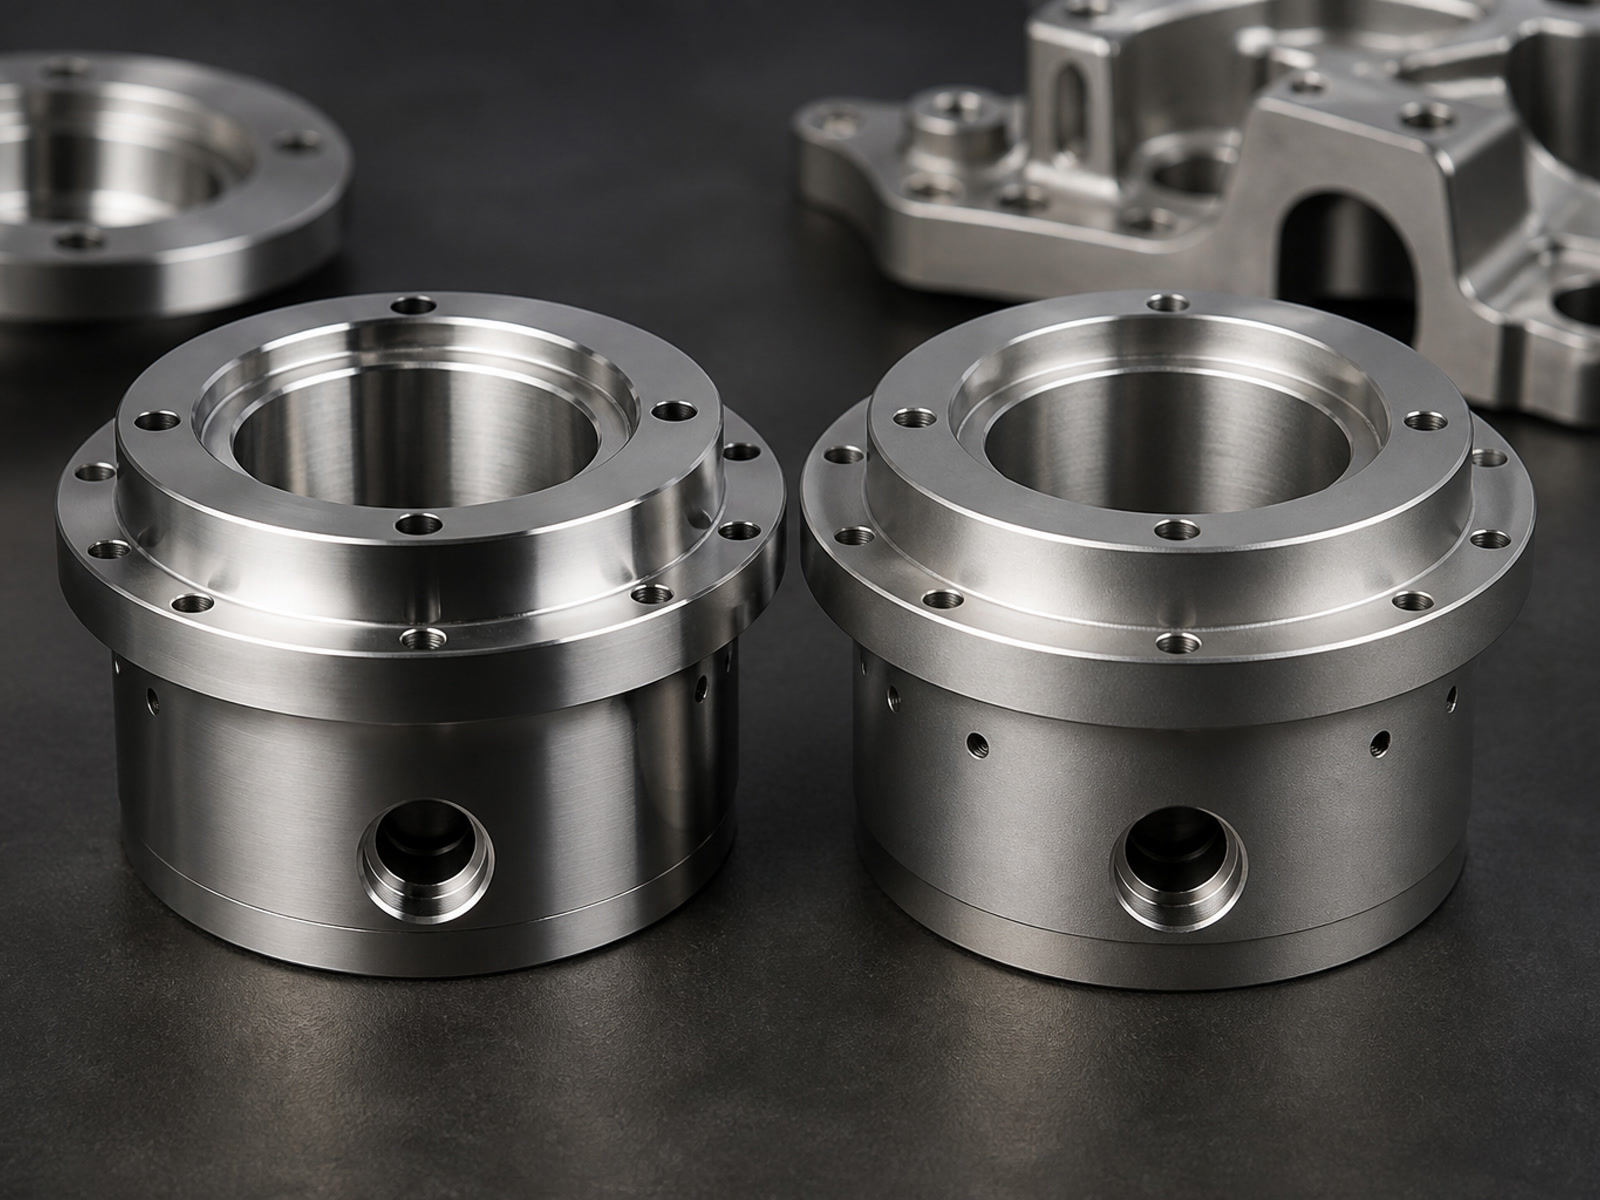
Why choose AXALLOY for Inconel vs Hastelloy parts
We are a Shenzhen-based CNC machining partner specializing in difficult-to-machine alloys. Our team supports international engineering, procurement and quality stakeholders from first article through stable, low-volume and repeat programs. If you need a supplier who understands manufacturability, risk control and documentation—not just the lowest unit price—we're built for you.
Difficult alloys, done right
Inconel 718/625, Hastelloy C-276/C-22 and more
Tight tolerances and complex geometries
3-, 4-, and 5-axis milling; turning; mill-turn; EDM; grinding
Engineering partnership
DFM feedback, tolerance review, fixture strategy, process definition
Inspection and traceability
FAI, dimensional reports, MTRs, CoC, special-process certificates
Procurement-friendly lead times
Prototypes in 5–10 business days; standard production in 10–20 business days; expedited service available
Markets served
North America, Europe, UK, Australia, New Zealand and advanced manufacturing hubs in Asia
Practical comparison: Inconel vs Hastelloy for precision machined parts
Both material families are nickel-based and tough to machine—but they solve different problems. We help your team select and manufacture the right grade for performance, cost and schedule.
Inconel
e.g., 625, 718
Strength and temperature
Exceptional high-temperature strength, oxidation resistance; common in hot sections, high-pressure environments
Typical use cases
Turbomachinery components, high-temperature fixtures, aerospace brackets, downhole equipment, high-pressure manifolds
Machining notes
Severe work-hardening and heat generation; requires rigid fixturing, conservative feeds/speeds, toolpath optimization, frequent tool changes; Inconel 718 often needs controlled heat treatment for stable dimensions
Hastelloy
e.g., C-276, C-22
Corrosion resistance
Outstanding resistance in aggressive, reducing and mixed chemical environments; excellent pitting/crevice resistance
Typical use cases
Chemical processing components, corrosive fluid manifolds, semiconductor wet-process hardware, marine and energy systems
Machining notes
Tough and "gummy"; demands sharp carbide, optimized chip control, flood coolant; careful deburring and surface finishing to maintain corrosion performance
Choosing between them
- • Pick Inconel for sustained high temperature, mechanical strength and oxidation resistance
- • Pick Hastelloy for extreme corrosion resistance in challenging chemistries
- • We evaluate your geometry, tolerances, surface requirements, inspection strategy and volume before defining the machining process
Difficult-alloy materials we machine
Our material expertise spans the full range of difficult-to-machine alloys used in demanding applications.
Core machining capabilities
CNC milling (3-, 4-, 5-axis)
Travel up to X 1,000 × Y 600 × Z 600 mm; table load up to 800 kg; up to 60 tools
Positioning accuracy ±0.005 mm; repeatability ±0.003 mm
Precision finish: Ra 0.8 μm; minimum internal corner radius ~R0.3 mm; minimum wall thickness ~0.5 mm
CNC turning and mill-turn
Turning: Ø500 mm × 1,000 mm length; bar up to Ø80 mm; ±0.005 mm tolerances
Mill-turn: up to 9 axes; Ø400 mm × 800 mm length; live tools to 12,000 rpm
Swiss turning
Small parts: Ø0.5–32 mm; length up to 300 mm; repeatability ±0.003 mm
EDM and precision grinding
Wire EDM: down to ±0.005 mm accuracy; Sinker EDM: min internal radius ~R0.05 mm
Grinding: surface/cylindrical/centerless; tolerances down to ±0.002 mm and Ra 0.2 μm
Tolerances and finishes
Dimensional
Standard ±0.010 mm
Precision down to ±0.005 mm
Angular
Standard ±0.5°
Precision ±0.1°
Position
Down to 0.010 mm
Flatness / Concentricity
Flatness down to 0.005 mm
Concentricity down to 0.008 mm
Surface finish
Machined Ra 1.6–0.8 μm; ground down to Ra 0.2 μm; EDM down to Ra 0.8 μm
Final tolerances and finishes depend on alloy, geometry, size, fixturing, inspection method and volume. We confirm achievable requirements during RFQ and DFM.
Engineering support and process control
- •Drawing review and DFM feedback for difficult features, thin walls and critical interfaces
- •Tolerance analysis and datum strategy for robust inspection plans
- •Fixture planning and machining-process development tailored to Inconel and Hastelloy behavior
- •Special processes: heat treatment, passivation, coating, deburring, marking, cleaning and assembly support
Inspection and documentation
- •CMM measuring range 700 × 1,000 × 600 mm; accuracy up to 1.8 + L/300 μm
- •Optical measurement accuracy ±0.002 mm; height gauge resolution 0.001 mm
- •Surface roughness range Ra 0.05–40 μm; hardness testing (Rockwell, Brinell, Vickers)
- •Controlled inspection environment; calibrated equipment
- •Documentation: MTR, Mill Test Certificate, CoC, FAI report, ballooned drawing, full dimensional report, surface roughness report, heat treatment and coating certificates, material/lot traceability
- •Custom inspection plans and project-specific quality records available
Industries and project profiles we serve
Industries
Aerospace, medical devices, semiconductor equipment, energy, oil & gas, marine, robotics, automation, precision industrial equipment
Companies
OEMs, Tier 1/2 suppliers, engineering firms, contract manufacturers, product-development teams
Best-fit projects
Complex geometry, thin walls, tight GD&T, demanding surfaces, difficult threads/holes; high-value prototypes; low-volume/high-mix production; repeat programs; supplier transfer and recovery projects
Not an ideal fit
Commodity parts purchased solely on lowest price, incomplete technical requirements, unverified certification demands or unauthorized component reproduction
Lead times, volumes and logistics
Prototype
5–10 business days
Standard production
10–20 business days
Expedited service
Available upon request
Minimum order
1 part
Volumes
1–10,000+ parts: prototype 1–20; low-volume 20–500; batch 500–10,000+
Global support
North America, Europe, UK, Australia, New Zealand and Asia
Example parts we machine
- •Valve bodies, nozzles, manifolds, fittings and threaded components
- •Impellers, blades and high-temperature structural brackets
- •Shafts, sleeves, bushings and precision plates
- •Semiconductor wet-process hardware and corrosion-critical inserts
- •Complex multi-feature rotational components (mill-turn)
How to request a quote (RFQ)
To quote Inconel vs Hastelloy parts accurately, we need complete technical inputs and your commercial expectations.
Please include:
- •2D drawings (PDF/DWG/DXF) with tolerances, GD&T and surface requirements
- •3D model (STEP/STP/IGES/X_T/X_B/SLDPRT/SAT)
- •Material grade (e.g., Inconel 718 vs Hastelloy C-276), heat treatment and special process specs
- •Quantities (prototype and/or production) and target delivery dates
- •Critical features and inspection documentation needed (FAI, dimensional report, CoC, MTR, etc.)
- •Any project-specific packaging or export requirements
Supported files
STEP, STP, IGES, IGS, X_T, X_B, SLDPRT, SAT, PDF, DWG, DXF, ZIP, RAR, JPG, PNG, TIFF
Maximum upload: 500 MB per RFQ
Units: millimeters and inches
Send us your RFQ
We'll review manufacturability, confirm achievable tolerances/finishes, propose the machining route and provide a risk-controlled quotation and schedule.
Our commitment
We evaluate material behavior, geometry, tolerances, surface requirements, inspection strategy and production volume before defining the machining process. You get dependable communication, controlled documentation and a supplier aligned with your engineering, procurement and quality expectations.
Ready to compare Inconel vs Hastelloy for your part and get a dependable machining route? Send your RFQ and drawings to AXALLOY Precision — we'll respond quickly with technical feedback and a clear plan from prototype through repeat production.