
CNC Machining for Difficult Alloys
Aerospace Inconel Parts CNC Machining (RFQ-Ready)
Aerospace Inconel parts often fail on the details: tool pressure causes distortion, heat builds up, threads tear, and dimensional variation shows up after inspection. At AXALLOY Precision (Shenzhen), we machine Inconel 718/625 and other difficult nickel alloys for engineering, procurement, and quality teams that need repeatable results, documented inspection, and controlled processes—from prototype validation to low-volume and repeat production.
If you want an RFQ that comes back with a clear process route, realistic tolerances, and the documentation you’ll need for release, send your drawing/model and requirements and we’ll quote accordingly.
Request an RFQWhat you get when you RFQ Aerospace Inconel Parts with AXALLOY
1) A machining plan that reduces scrap risk in Inconel
What you get: fewer surprises between prototype and repeat orders.
We review geometry, tolerances, surface requirements, inspection strategy, and volume before defining the process—so the quoted route matches how the part will actually be produced.
2) Tolerance and GD&T support built into the quote
What you get: early feedback on what’s stable, what’s sensitive, and what needs a fixture/sequence change.
For Inconel aerospace components with thin walls, critical interfaces, or positional tolerances, we can provide DFM and tolerance review so your team can release drawings with fewer revisions.
3) Fewer setups for stronger feature relationships
What you get: better concentricity/position consistency because features are created in fewer clampings.
With 3/4/5-axis milling plus turning and mill-turn, we support parts where alignment between milled and turned features matters (ports, bores, sealing faces, mating datums).
4) Inspection evidence that supports quality approval
What you get: records that help supplier onboarding, FAI, and in-house receiving.
We support material traceability, first article inspection, dimensional reports, and project-specific documentation.
5) Lead times that help you hit engineering and build gates
What you get: prototypes in time for design verification and build schedules—reducing schedule risk.
Prototype and expedited options are designed to help you validate fit/function earlier, then lock a stable route for low-volume or repeat production.
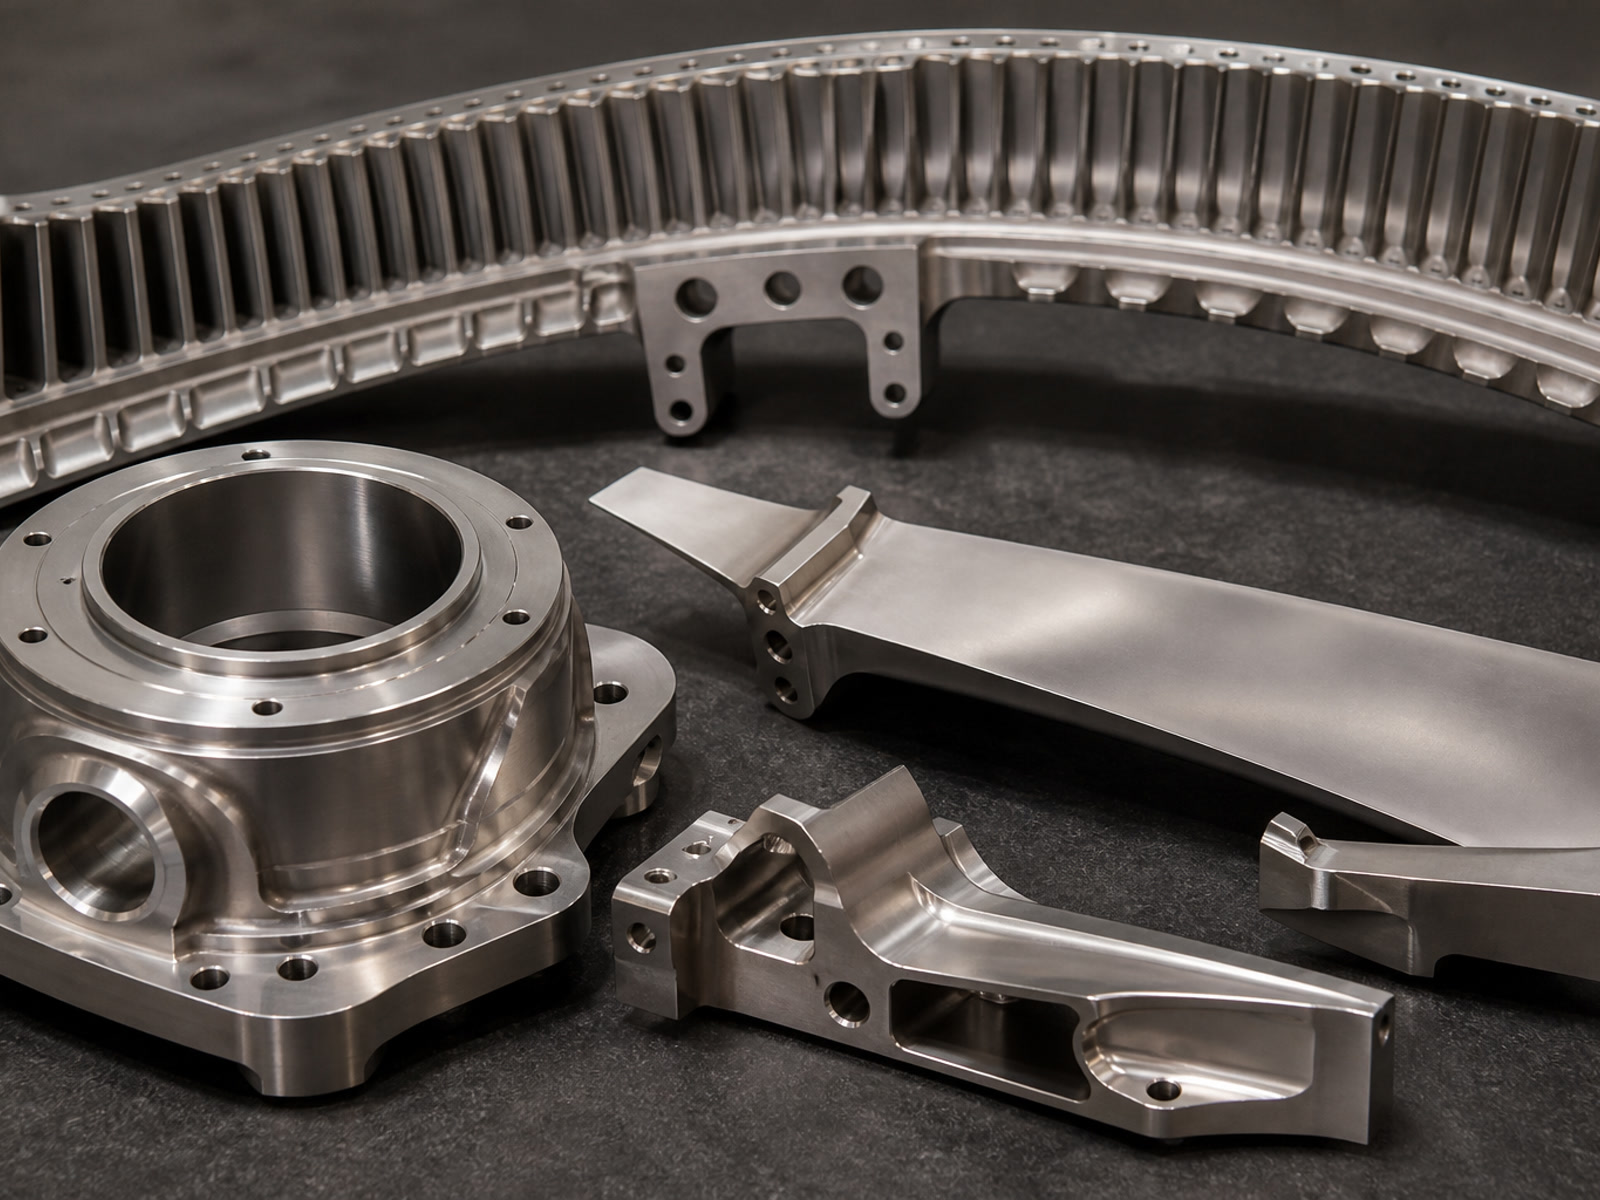
Aerospace Inconel Parts we commonly support
Brackets, housings, manifolds, interfaces with tight positional control
Impellers/blades and complex 5-axis contoured components
Shafts, sleeves, bushings, nozzles, fittings, threaded components
Thin-wall parts, deep pockets, critical sealing faces, difficult holes/threads
Parts requiring EDM features, grinding on fits/sealing surfaces, or special process coordination
Capabilities for Inconel aerospace components
General machining capability (typical)
| Supported production volume | 1–10,000+ parts |
| Prototype quantity | 1–20 parts |
| Low-volume production | 20–500 parts |
| Batch production | 500–10,000+ parts |
| Standard dimensional tolerance | ±0.010 mm |
| Precision dimensional tolerance | ±0.005 mm |
| Position tolerance | down to 0.010 mm |
| Flatness | down to 0.005 mm |
| Concentricity | down to 0.008 mm |
| Standard surface finish | Ra 1.6 μm |
| Precision machined finish | Ra 0.8 μm |
| Ground surface finish | down to Ra 0.2 μm |
| Minimum wall thickness | 0.5 mm |
| Minimum machined hole diameter | Ø0.5 mm |
| Minimum thread size | M1.0 |
| Standard lead time | 10–20 business days |
| Prototype lead time | 5–10 business days |
| Minimum order quantity | 1 part |
CNC milling (3/4/5-axis)
| Machining types | 3-axis, 4-axis, 5-axis CNC milling |
| Max 3-axis part size | 1,000 × 600 × 600 mm |
| Max 4-axis part size | Ø500 × 800 mm |
| Max 5-axis part size | Ø500 × 400 mm |
| Positioning accuracy | ±0.005 mm |
| Repeatability | ±0.003 mm |
| Milling tolerance | down to ±0.005 mm |
| Min internal corner radius | R0.3 mm |
| Supported operations | facing, contouring, pocketing, drilling, tapping, boring, thread milling |
Turning / Mill-turn
| Parameter | Turning | Mill-turn |
|---|---|---|
| Max diameter | Ø500 mm | Ø400 mm |
| Max length | 1,000 mm | 800 mm |
| Typical tolerance | down to ±0.005 mm | ±0.008 mm (typical) |
| Concentricity | down to 0.008 mm | positioning accuracy ±0.005 mm |
| Configuration | 2-axis + live-tool | main/sub spindle, C/Y, live tooling, up to 9 axes |
EDM and grinding (for features milling can’t hold economically)
| Process | What it helps you achieve | Standard capability |
|---|---|---|
| Wire EDM | narrow slots, sharp internal corners, precise profiles in Inconel | accuracy down to ±0.005 mm; Ra down to 0.8 μm |
| Sinker EDM | deep cavities, ribs, blind features, small internal radii | min internal corner radius R0.05 mm; Ra down to 0.4 μm |
| Precision grinding | bearing fits, sealing surfaces, stable flatness/roundness | tolerance down to ±0.002 mm; Ra down to 0.2 μm |
Materials: Inconel and related difficult alloys
We regularly support nickel-based superalloys including:
- Inconel 718 / 625 (common for aerospace hardware)
- Inconel 600/601/690/706/725/X-750
- Hastelloy C-22 / C-276, Monel 400/K-500, Haynes 188/230/282
- Titanium Grades 2/5/23, 15-5 PH / 17-4 PH, duplex 2205 / super duplex 2507, A286, MP35N
If you have a specified heat/lot or certification requirement, include it in the RFQ so we can align material traceability and documentation from the start.
Inspection & documentation you can request
Inspection capabilities (selected)
| CMM measuring range | 700 × 1,000 × 600 mm |
| CMM accuracy | up to 1.8 + L/300 μm |
| Optical measurement accuracy | ±0.002 mm |
| Surface roughness measurement | Ra 0.05–40 μm |
| Thread inspection | thread gauges + optical measurement |
| Environment | temperature-controlled inspection room |
Documentation options
- Material Test Report / Mill Test Certificate
- Certificate of Conformance (CoC)
- First Article Inspection (FAI) report
- Ballooned drawing + full dimensional inspection report
- Surface roughness report
- Heat treatment / coating certificates (when applicable)
- Material and lot traceability, special process records
What to send for an accurate Aerospace Inconel Parts RFQ
To return a quote that your engineering, procurement, and quality teams can actually release, send:
- 13D model + 2D drawing (STEP/IGES/X_T + PDF/DWG/DXF)
- 2Material grade (e.g., Inconel 718) and any required certs/standards
- 3Quantity (prototype and expected repeat volumes)
- 4Critical features (GD&T callouts, datums, sealing surfaces, threads)
- 5Surface finish requirements and any special processes (heat treat, passivation, coating)
- 6Target date and shipping destination
- 7Required documentation (FAI, full dimensional, traceability, etc.)
Supported file formats
STEP/STP, IGES/IGS, X_T/X_B, SLDPRT, SAT; PDF/DWG/DXF.
Max upload size: 500 MB per RFQ.
Request an RFQ (Aerospace Inconel Parts)
Share your drawings/models and requirements, and we will respond with:
- A priced quotation aligned to your tolerance, surface, and documentation needs
- A manufacturing approach (setups, key risks, inspection plan) suitable for repeatability
- A lead-time plan matched to prototype validation or production scheduling
Send your RFQ package to AXALLOY Precision and include any program constraints (export packaging, identification/marking, cleanliness, assembly support) so the quote reflects your real release conditions.
Request a Quote
Tell us about your component requirements and material challenges.