
AXALLOY Precision
Precision EDM Components
AXALLOY Precision provides Wire EDM and Sinker EDM solutions for complex, high-value components in difficult-to-machine alloys. Based in Shenzhen and serving international engineering, procurement and quality teams, we support prototype development through controlled, low-volume and repeat production.
Our EDM services integrate with multi-axis milling, turning, precision grinding and comprehensive inspection to deliver dimensionally precise, burr-free components with reliable documentation.
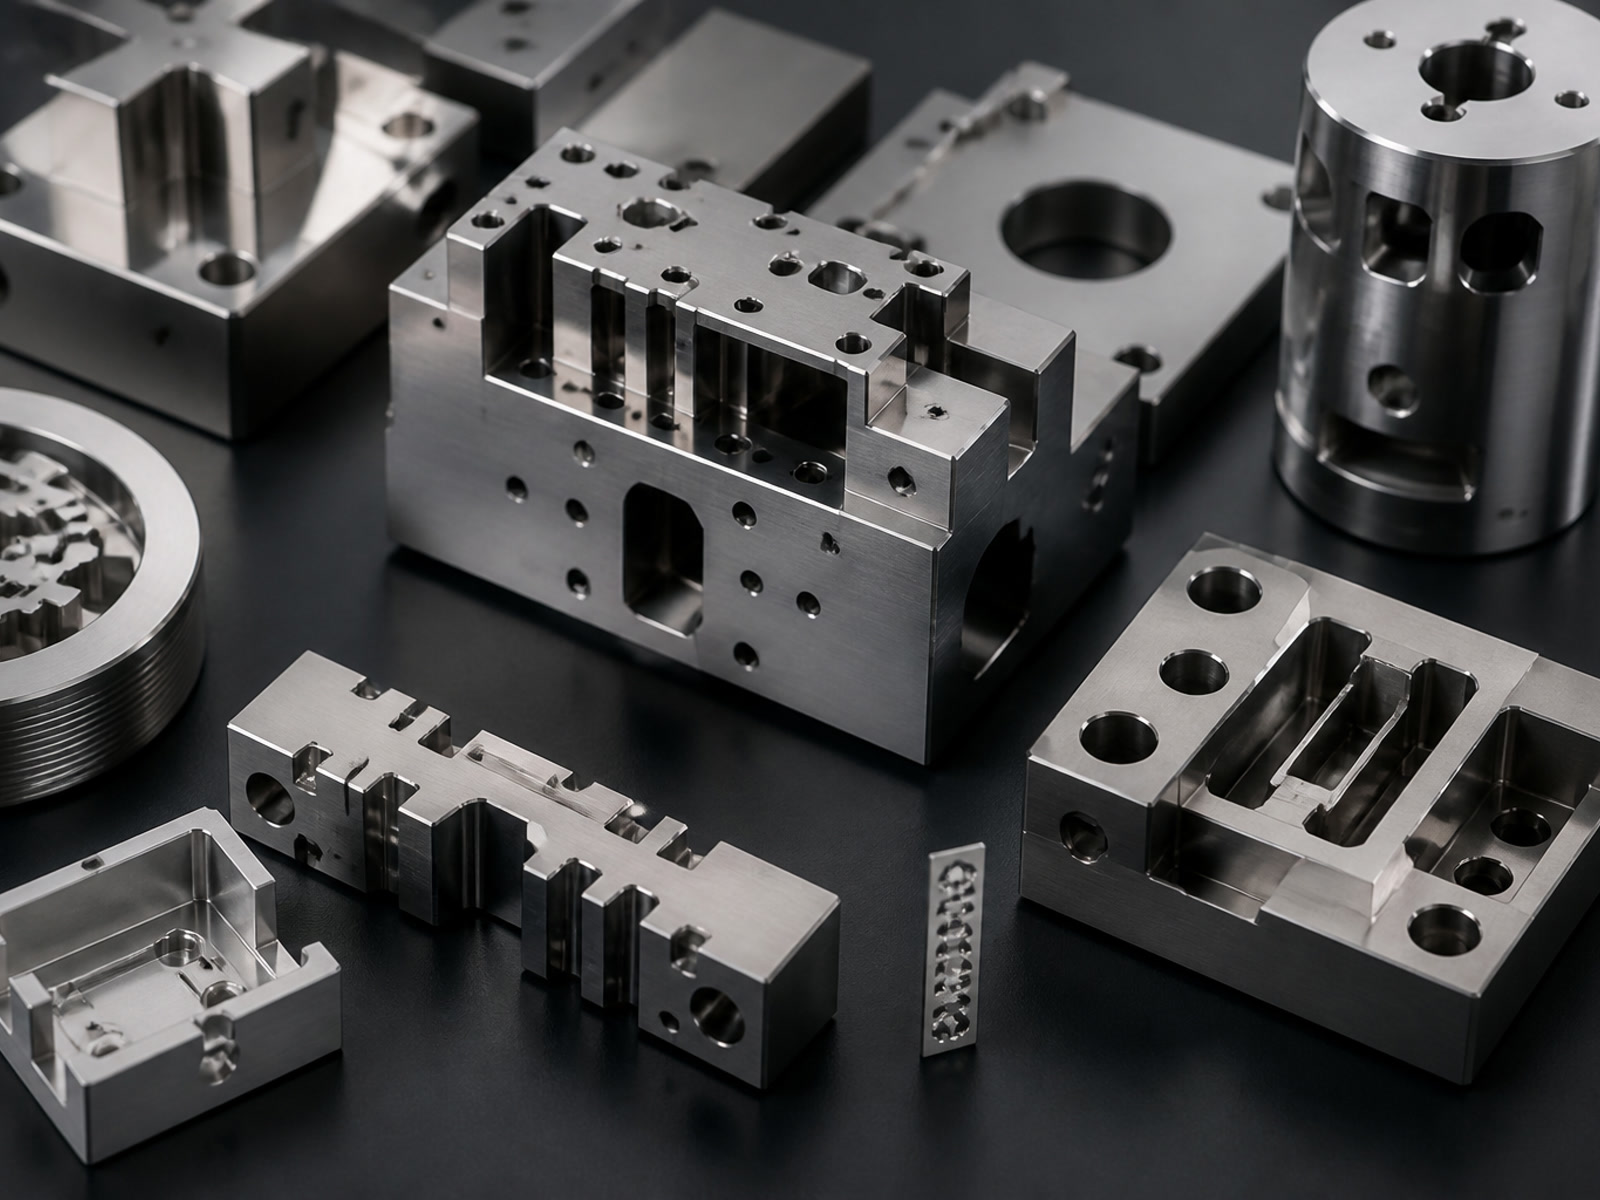
What We Deliver
- Tight-tolerance profiles, slots, dies and sharp internal corners not achievable by conventional cutting tools
- Stable machining of nickel superalloys, titanium, precipitation-hardening stainless steels, duplex and cobalt alloys
- Proven process control from DFM and fixture planning to inspection strategy and documentation
- Prototype to production support with dependable communication and traceability
When EDM Is the Right Choice
- Sharp internal corners and very small internal radii
- Extremely fine slots, thin ribs and narrow profiles
- Hard, tough or heat-resistant alloys (Inconel, Hastelloy, titanium, PH stainless)
- Delicate geometries where cutting forces would distort thin walls
- Burr-free edges and minimal distortion requirements
- Final sizing of hardened or heat-treated parts
EDM Capabilities at a Glance
Wire EDM (WEDM)
- Max workpiece size
- 600 × 400 × 300 mm
- Max workpiece weight
- 500 kg
- Wire diameter
- Ø0.10–0.30 mm
- Min cutting width (kerf)
- 0.15 mm
- Cutting accuracy
- down to ±0.005 mm
- Repeatability
- ±0.003 mm
- Max cutting taper
- ±30°
- Surface finish
- down to Ra 0.8 μm
- Max cutting thickness
- 300 mm
Ideal for: narrow slots, precision profiles, punches, dies, inserts, sharp internal corners
Sinker EDM (Die-Sinking)
- Max workpiece size
- 500 × 350 × 300 mm
- Max workpiece weight
- 800 kg
- Positioning accuracy
- ±0.005 mm
- Repeatability
- ±0.003 mm
- Surface finish
- down to Ra 0.4 μm
- Min internal corner radius
- R0.05 mm
- Max machining depth
- 250 mm
Ideal for: deep cavities, ribs, blind features, fine radii and complex internal profiles
Materials We EDM
We maintain stable, documented processes across the most demanding alloy families used in aerospace, medical, energy and semiconductor applications.
Tolerances & Surface Finish
- Dimensional accuracy: down to ±0.005 mm
- Repeatability: ±0.003 mm
- Wire EDM finish: down to Ra 0.8 μm (multi-pass skim)
- Sinker EDM finish: down to Ra 0.4 μm (fine finishing)
- Post-process grinding: down to Ra 0.2 μm and ±0.002 mm
Typical Precision EDM Components
From single prototypes to controlled production runs, we machine components that demand precision and material expertise.
Dies, punches, wear plates and precision inserts
Surgical and implant tooling features, instrument details
Micro-slots, fine nozzles, metering orifice details
Valve seats, sealing profiles and precision interfaces
Turbine/impeller details, dovetails and fir-tree profiles
Semiconductor tooling features and wafer-side profiles
Complex connectors, splines and keyways
Internal gear forms and intricate profiles
Integrated Processes
Our EDM services are part of a fully integrated precision machining environment, giving you strong feature relationships and fewer setups.
Upstream Machining
3-, 4- and 5-axis milling; turning and mill-turn; Swiss turning
Special Processes
EDM, precision grinding, heat treatment, passivation, coating, deburring, marking, cleaning and assembly support
Inspection & Documentation
FAI, full dimensional reports, material traceability and project-specific quality records
Inspection & Quality Documentation
Calibrated Inspection Equipment
- CMM range: 700 × 1,000 × 600 mm
- CMM accuracy: up to 1.8 + L/300 μm
- Optical measurement: ±0.002 mm
- Height gauge resolution: 0.001 mm
- Surface roughness: Ra 0.05–40 μm
- Hardness: Rockwell, Brinell, Vickers
Temperature-controlled inspection room and calibrated equipment
Available Documentation
- Material Test Report
- Mill Test Certificate
- Certificate of Conformance
- First Article Inspection Report
- Ballooned Drawing
- Full Dimensional Report
- Surface Roughness Report
- Heat Treatment & Coating Certificates
- Material & lot traceability
- Special-process records
- Inspection photos (on request)
- Custom quality documentation on request
Design for EDM (DFM) Guidelines
Start Holes for Wire EDM
Provide a start hole where possible. Typical practical range Ø0.2–2.0 mm; we can prepare start holes via drilling or pre-machining when not defined on drawing.
Minimum Kerf / Slot Width
≥0.15 mm (wire diameter and strategy dependent).
Corner Radii
Wire EDM: internal corners can be extremely sharp relative to tool-machined features; specify minimum radii if intentional. Sinker EDM: minimum internal radius down to R0.05 mm with appropriate electrode strategy.
Tapers & Draft
Wire EDM supports up to ±30° taper; call out taper direction and datum references.
Wall Thickness
For unsupported walls, ≥0.5 mm is recommended; thinner features may be feasible with process controls—flag as critical.
Tolerance Stacking
Identify critical datums and GD&T to align machining, EDM and inspection strategies.
Surface Integrity
EDM leaves a thin recast layer; specify if post-EDM polishing, stoning or light grind is required for fatigue-critical or sealing surfaces.
Fixturing & Access
Allow clamping allowances and flush paths; avoid obstructed cavities that limit dielectric flow.
Threads & Forms
For extremely small or interrupted internal forms, consider pre-machining followed by EDM finishing; we also support thread milling/tapping for hybrid processes.
Documentation
Annotate critical features, inspection points and surface requirements on the 2D drawing to reduce ambiguity.
Need DFM feedback? We provide drawing review, tolerance review, fixture planning and machining-process development before production release.
Get DFM FeedbackWho We Serve
Industries
Aerospace, medical devices, semiconductor equipment, energy, oil & gas, marine, robotics, automation and precision industrial equipment
Company Types
OEMs, Tier 1/2 suppliers, engineering firms, contract manufacturers, product-development teams
Decision-Makers
Mechanical/design/manufacturing engineers, sourcing and commodity managers, SQEs and quality managers
Best-Fit Projects
- Complex geometry, thin walls, tight GD&T, demanding surfaces, difficult holes/threads
- High-value prototypes, low-volume/high-mix production, repeat programs, supplier transfers
- Parts requiring certification, FAI, dimensional reports, special-process records or export-ready packaging
Why AXALLOY for Precision EDM
Difficult-Alloy Expertise
Stable processes for Inconel, Hastelloy, titanium, PH stainless, duplex, cobalt and specialty metals
Integrated Precision
Combine multi-axis milling/turning, EDM and grinding for strong feature relationships and fewer setups
Process Control & Traceability
Robust fixturing, in-process checks, controlled documentation and inspection evidence
Engineering Support
Proactive DFM, tolerance consultation and inspection planning aligned to your critical features
Communication & Reliability
Responsive updates, clear commitments and predictable delivery
Lead Times & Volumes
- Prototype lead time
- 5–10 business days
- Standard lead time
- 10–20 business days
- Expedited service
- Available on request
- Quantities
- 1-off to 10,000+ parts
File Formats & RFQ Inputs
- 3D CAD
- STEP/STP, IGES/IGS, X_T/X_B, SLDPRT, SAT
- 2D drawings
- PDF, DWG, DXF
- References
- JPG, PNG, TIFF
- Compressed
- ZIP, RAR
- Max upload size
- 500 MB per RFQ
- Drawing units
- Metric (mm) & Imperial (in)
For the Fastest, Most Accurate Quote, Include:
- 2D drawing with GD&T and critical features flagged
- 3D model
- Material and heat-treat condition
- Quantities and target delivery date
- Required documentation (MTR, CoC, FAI, full inspection)
- Special surface, cleanliness or packaging requirements
Project Workflow
RFQ Submission
Submit your drawings and models; we review for DFM and manufacturability.
Process Plan
We develop a process plan with fixture strategy and inspection approach.
Quote
Receive a clear quote with lead time, price and documentation scope.
Sample / FAI
Sample or First Article Inspection as required, with customer approval.
Controlled Production
Production runs with in-process inspection at every critical step.
Final Inspection & Shipment
Final inspection, complete documentation pack and shipment.
Frequently Asked Questions
Can you EDM hardened or heat-treated parts?
Yes. EDM is well-suited to hardened and high-temperature alloys. If recast removal is required, we can follow with fine grinding or polishing.
How small can my slot or internal corner be?
Wire EDM kerf is typically ≥0.15 mm; for internal radii, Sinker EDM can achieve down to R0.05 mm with the right electrode and strategy.
What surface finish can I expect?
Wire EDM down to Ra 0.8 μm (multi-pass skim); Sinker EDM down to Ra 0.4 μm. Precision grinding to Ra 0.2 μm is available when specified.
Do you provide inspection and traceability?
Yes. We offer MTRs, CoC, FAI, ballooned drawings, full dimensional reports and special-process records with calibrated equipment in a controlled inspection environment.
Which industries and regions do you serve?
We regularly support aerospace, medical, semiconductor and precision industrial projects across North America, Europe, the UK, Australia, New Zealand and advanced Asian markets.
Get a Quote
Ready for dependable, precision EDM components? Share your drawings and models to receive DFM feedback and a clear, controlled route to production.
- Upload your files (up to 500 MB per RFQ)
- Specify materials, quantities and required documentation
- Indicate prototype or production timing and any expedited needs
Need DFM feedback? We provide drawing review, tolerance review, fixture planning and machining-process development before production release.
AXALLOY Precision — Precision Machining for Difficult Alloys.
Request a Quote
Tell us about your component requirements and material challenges.