
Duplex Stainless Steel Machining
AXALLOY delivers high-precision CNC milling, turning, and multi-axis machining for Duplex 2205 and Super Duplex 2507 alloys. Engineered for mission-critical offshore, marine, chemical, and pressure-boundary systems, our controlled processes prevent work-hardening and deliver dimensional tolerances down to ±0.005 mm with complete metallurgical traceability.
Duplex Machining Benchmarks
- Positioning & Tolerance
- Down to ±0.005 mm
- Standard Alloys
- 2205 / 2507 / Ferralium
- Surface Finish
- Down to Ra 0.4 μm
- Quality Validation
- EN 10204 3.1 & CMM FAIR
Duplex Component Manufacturing Articles & Services
Explore specialized turning, milling, and finished sub-assembly processes managed by AXALLOY.
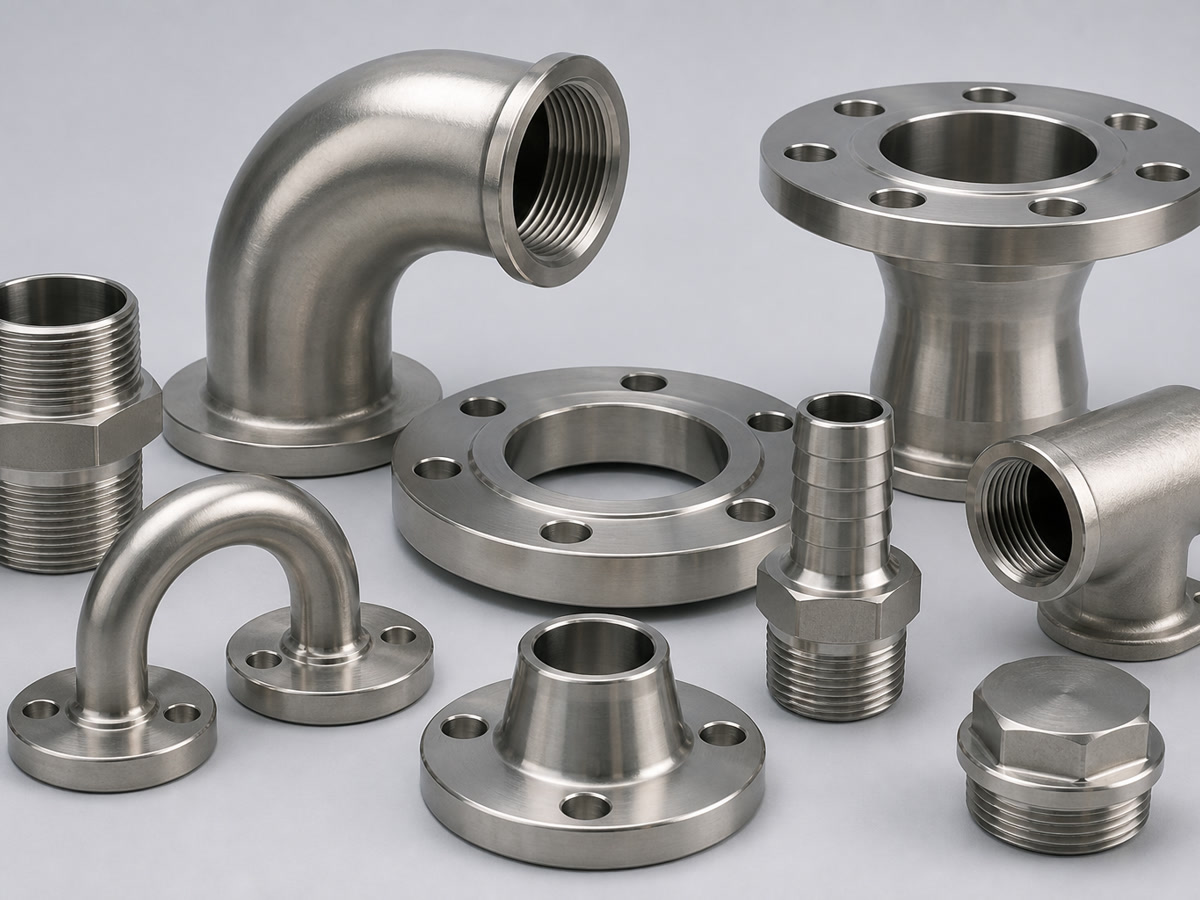
Duplex Marine Parts CNC Machining for Difficult Alloys
Duplex Marine Parts CNC machining: tight-tolerance Duplex/Super Duplex stainless components, prototype to low-volume, with material traceability. Get a quote.
View details →Duplex & Super Duplex Machining Capabilities
Because duplex stainless steels exhibit double the yield strength of conventional austenitic grades and work-harden rapidly, AXALLOY applies high-pressure through-spindle coolant, custom-ground negative-rake carbide inserts, and rigid multi-axis fixturing to eliminate chatter and maintain micro-inch surface finishes.
CNC Multi-Axis Milling
3-axis, 4-axis, and 5-axis simultaneous milling for complex bodies, valve blocks, impellers, and manifolds. Travels up to 1,000 × 600 × 600 mm with positional repeatability within ±0.003 mm.
Turn-Mill & Swiss Turning
Twin-spindle, live-tooling turn-mill centers for shafts, threaded couplings, and seal housings up to Ø500 mm. Swiss CNC capability down to Ø0.5 mm for high-precision instrumentation hardware.
Wire EDM & Grinding
Sub-micron wire cutting for deep valve sealing slots, tight keyways, and sharp internal corners where rotary tooling deflects. Cylindrical and surface grinding to Ra 0.2 μm.
| Specification Element | Duplex 2205 (EN 1.4462) | Super Duplex 2507 (EN 1.4410) | AXALLOY Process Control |
|---|---|---|---|
| Yield Strength (0.2%) | ≥ 450 MPa | ≥ 550 MPa | Rigid hydraulic chucking to prevent deflection |
| Machinability Rating | Approx. 45% (vs. AISI B1112) | Approx. 35% (vs. AISI B1112) | Constant chip load, positive rake geometry |
| Critical Tolerances | ±0.005 mm | ±0.005 mm | Climate-stabilized in-process CMM inspection |
| Thermal Distortion Strategy | Moderate thermal expansion | Low thermal conductivity | 70-bar high-pressure flood coolant delivered at tool tip |
How AXALLOY Eliminates Work-Hardening & Thermal Drift
Duplex alloys are prone to immediate work-hardening when tool dwell occurs or when dull cutting edges rub against the cut zone. Our multi-axis CNC programs follow strictly enforced production parameters developed exclusively for austenitic-ferritic microstructures:
- ✓ Never Dwelling in Cut: Zero-dwell feeds prevent surface glazing during turning, threading, and deep pocketing.
- ✓ High-Pressure Coolant (HPC): Through-spindle delivery breaks tough, continuous ribbon chips and flushes heat away from tool edges.
- ✓ Dedicated Coated Carbides: TiAlN and AlCrN physical-vapor-deposited coatings preserve cutting edge sharpness under heavy shear stresses.
- ✓ Stress-Relief Cycles: Rough-machining allowances followed by intermediate resting cycles to guarantee geometric stability across finished thin walls.
Quality Documentation Package
Every production release of Duplex components is matched with complete certification records to guarantee audit readiness for marine, subsea, and petrochemical installations:
Request a Machining Quote for Duplex Stainless Steel
Send your CAD models (STEP, IGES, X_T) and 2D drawings (PDF with GD&T notes). The AXALLOY technical engineering team will review manufacturability, cycle times, and alloy availability to deliver a competitive proposal within 24 hours.
Request a Quote
Tell us about your component requirements and material challenges.